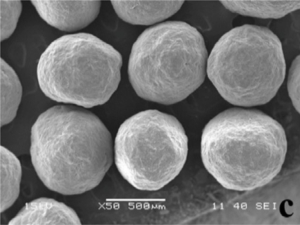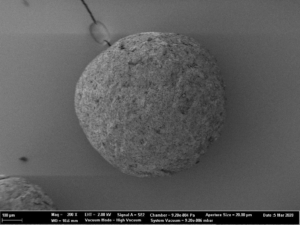
A pharmaceutical microcrystalline cellulose pellet is a small spherical agglomerate made of 100 % microcrystalline cellulose as a chemically inert material. Pellets are used as an excipient for tablet manufacture. Narrow particle size distributions are achieved with current production technologies. From a galenic point of view, an ideally defined and smooth surface speaks for the use of pellets in pharmaceutical formulations. In addition, pellets as a carrier system for active ingredients show particle size-dependent properties, such as fast and reproducible gastric passage, as well as uniform distribution in the respective section of the gastrointestinal tract during passage. Pellets are used in pharmaceutical formulations targeting oral dosage formas, such as capsules, MUPS (Multiple Unit Pellet System), or tablets.

Posts

MCC pellets under rheological investigation-thumbnail

MCC pellets under rheological investigation

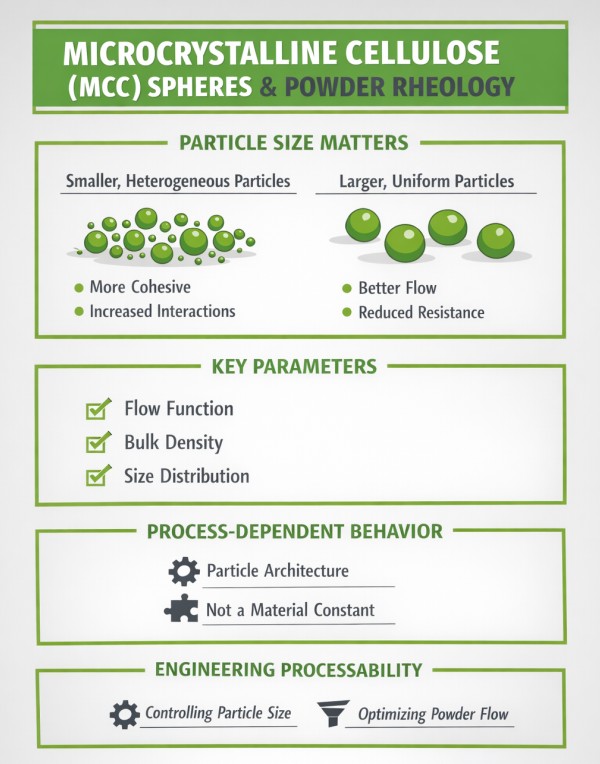
MCC pellets under rheological investigation are ideal model spheres for studying powder behavior. In this study, we revisit the work of V. Mohylyuk and R. Dattani to analyze the effect of pellet size on powder properties. Understanding how pellet size influences flow and handling is essential for optimizing powder performance. Moreover, investigating size variations helps improve material processing and formulation strategies. By focusing on these aspects, researchers can better predict and control the behavior of MCC spheres in different applications.

Rheological behavior has a deep impact

The rheological behavior of powders greatly affects pharmaceutical formulations and processing steps. In particular, when studying MCC pellets under rheological investigation, powder rheology becomes a key area of focus. Typically, powders behave as solids under static conditions; however, they can fluidize under certain circumstances. Consequently, fluidization is widely used in pharmaceutical processes because it enables controlled and uniform coating or layering of starter beads with drugs and functional excipients. Moreover, while fluid behavior in liquids depends on inter- and intra-molecular interactions, network bonds, and temperature, powder fluidization primarily relies on micro-particular properties such as particle size, surface characteristics, and flowability. In addition, the exact gas speed and volume required for powder fluidization must be carefully adjusted for each system. Therefore, a thorough analysis of the powder is essential to achieve precise control and optimal performance.

Materials: MCC pellets

CELLETS®

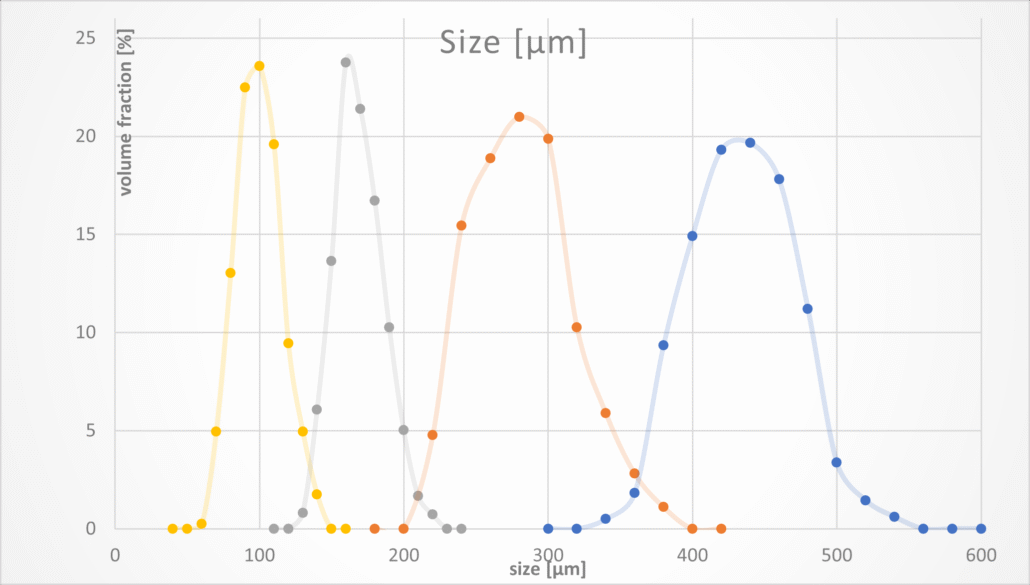
In this study, CELLETS® are used for the investigation. These pellets consist of Microcrystalline Cellulose, featuring a smooth surface, high sphericity, and minimal friability. Due to these properties, CELLETS® are popular as starter beads in pharmaceutical formulations and are ideal model spheres for rheological studies. Four types—CELLETS® 90, CELLETS® 100, CELLETS® 200, and CELLETS® 350—were examined, with size distributions ranging from 90 µm to 500 µm. The D50 values for these types vary between 94 µm and 424 µm. The specific size distribution of each CELLETS® type is summarized in Table 1.

Type Particle size distribution (≥ 85 %)
CELLETS® 90 60-100 µm
(250/150)
CELLETS® 100 100-200 µm
(150/80)
CELLETS® 200 200-355 µm
(80/50)
CELLETS® 350 350-500 µm
(50/35)

Table 1: Particle size distribution of selected MCC spheres.
 

MCC pellets under rheological investigation

Characterization Methods for MCC Pellets Under Rheological Investigation

First, we measured the particle size distribution of MCC pellets under rheological investigation using optical digital microscopy (Keyence VHX 600). This approach provides precise and reliable data on pellet dimensions, which is essential for understanding their flow and handling properties.

Next, we applied standard pharmacopoeia methods to determine bulk and tapped density, as well as flow rate using a gravitational funnel. In addition, we analyzed the dynamic angle of repose and dynamic cohesivity index with a rotating drum tester (GranuDrum). Furthermore, we used a powder rheometer (FT4 Powder Rheometer) to evaluate basic flowability energy, specific energy, aerated energy, permeability, and compressibility. Altogether, these measurements give a comprehensive understanding of MCC pellets under rheological investigation and offer detailed insights into their performance in pharmaceutical applications.

Results of the rheological investigations

Figure 1 presents the particle size distribution of MCC pellets under rheological investigation, as measured with an optical digital microscope.
Mohylyuk 2022 MCC pellets under rheological investigation image 1

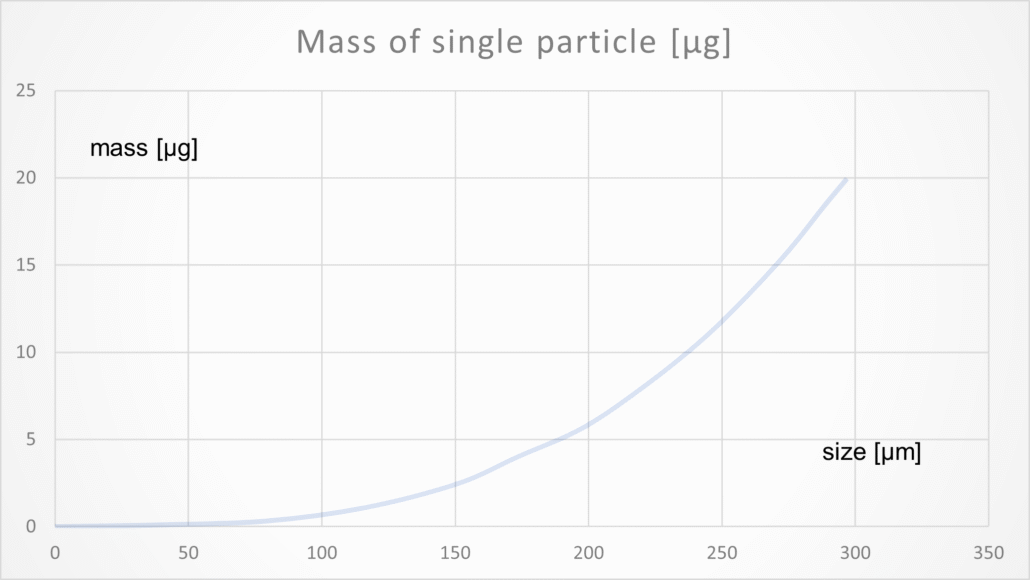
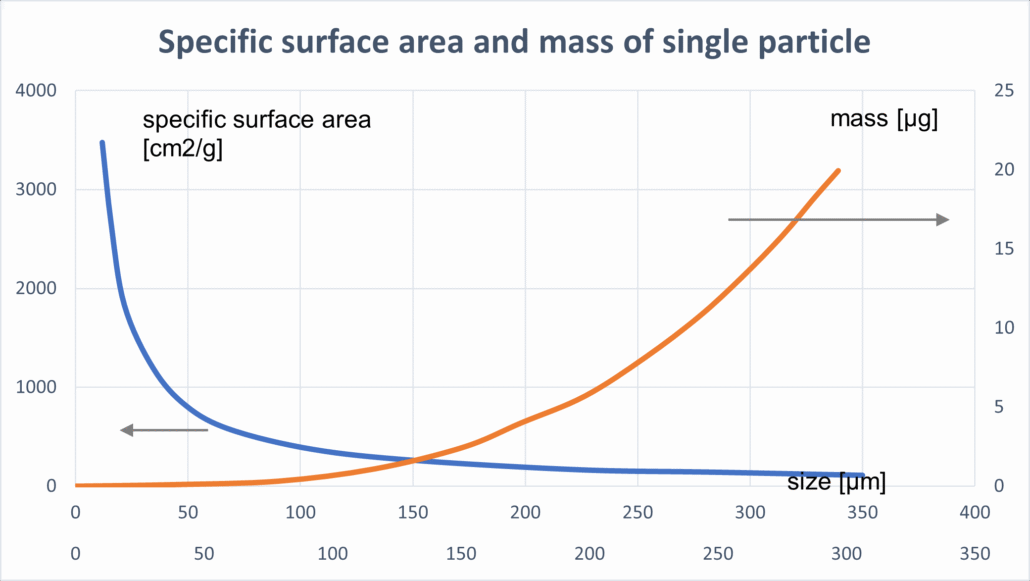
With increasing particle size the apparent specific surface area (fig. 2) decreases obviously. Hence, a decrease in pellet size, allow an expectation in increase in mechanical interlocking.
Mohylyuk 2022 MCC pellets under rheological investigation image 2
specific surface area

With increasing particle size, the bulk and tapped density of CELLETS® increases; however, the densification kinetics remained approximately the same for all pellet sizes (Fig. 3). Moreover, a few periodic oscillations significantly influenced the density of the pellets, highlighting subtle variations in their behavior.

density

With increasing particle size the compressibility decreases (fig. 4). The applied force was identical for all pellets sizes. Worsening packing efficiency.

Mohylyuk 2022 MCC pellets under rheological investigation image 4 compressibility

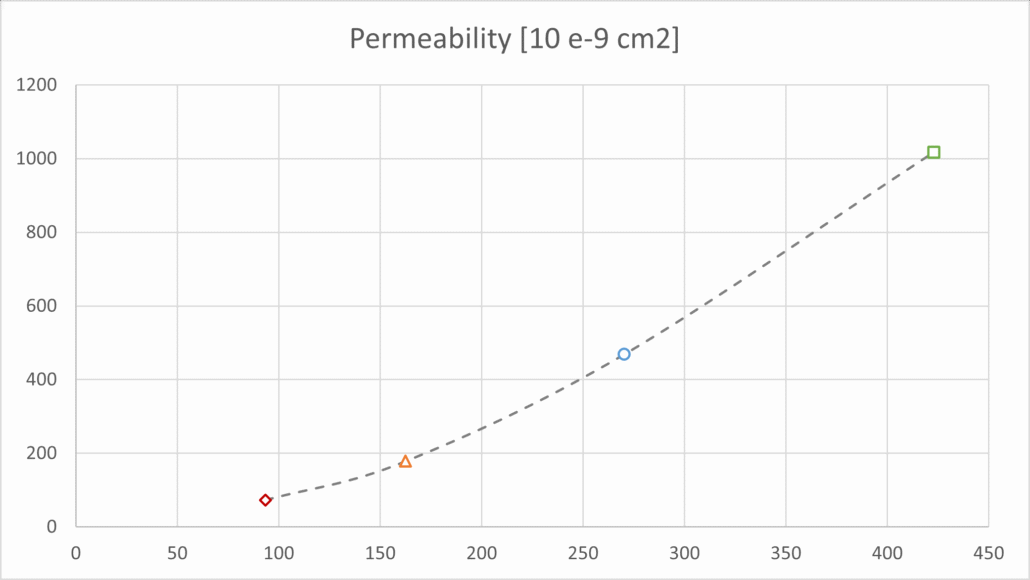
With increasing particle size the permeability increases while applying the same force for all pellet types. (fig. 5). increase in voids between particles.
permeability

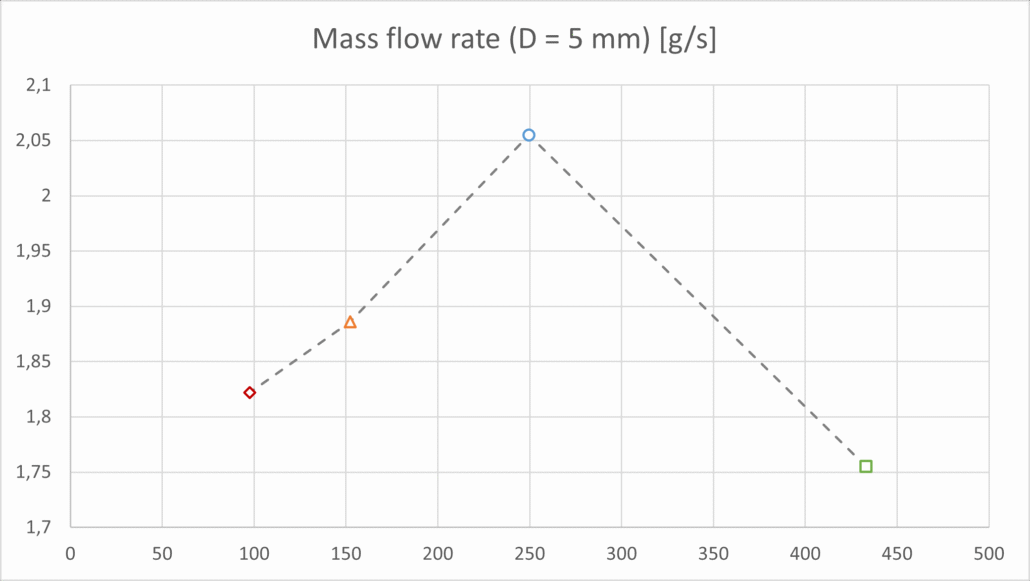
The gravitational funnel method suggests an absence of correlation between the mass flow rate and pellet size or specific surface area (fig. 6).
mass flow rate

Analyzing the dynamic angle of repose

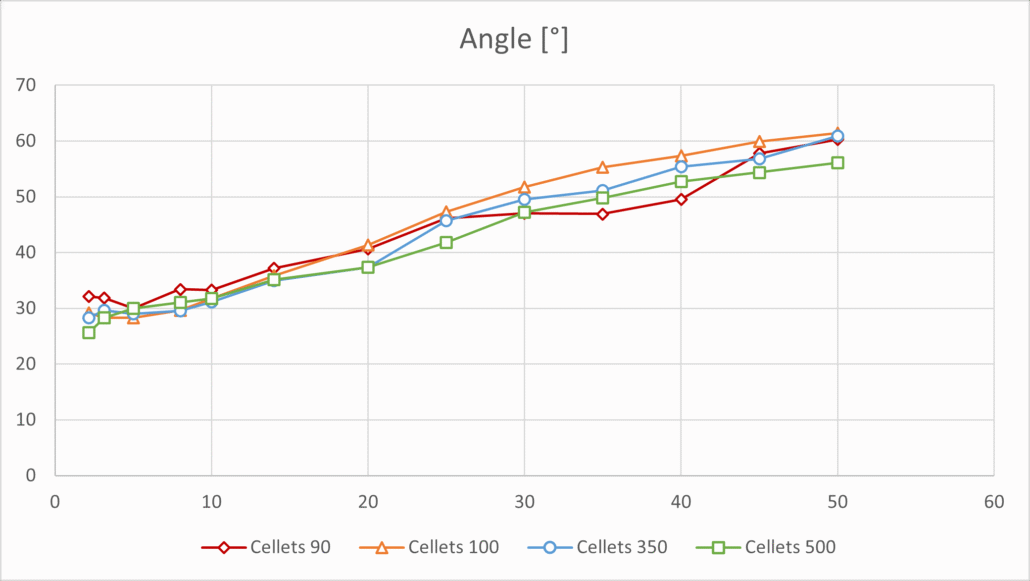
We analyzed the dynamic angle of repose to evaluate the powder flow of MCC pellets under rheological investigation. All pellet sizes showed similar behavior: as the rotation speed increased, the angle of repose rose almost linearly. The measurements for all pellet types formed a funnel shape within the range of analytic errors (Fig. 7). These results clearly characterize the dynamic flow ability of the powders.
Mohylyuk 2022 MCC pellets under rheological investigation image 7 angle

With increasing particle size the specific energy decreases (fig. 8). The level of interlocking and friction between powder particles decreased, the flowability increased.
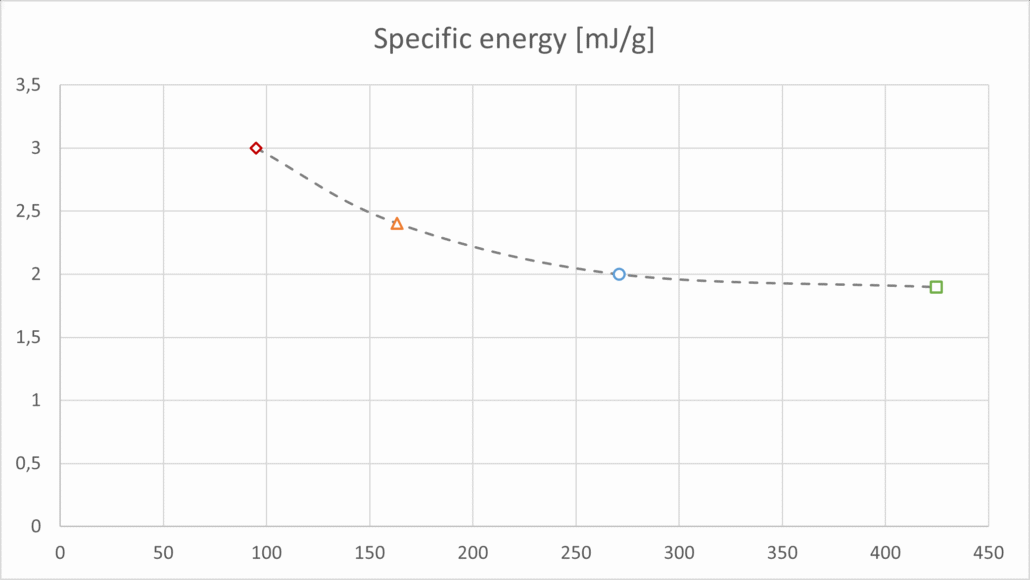
Image 8 specific energy

With increasing particle size the basic flowability energy decreases (fig. 9). the flowability in a constrained environment increased.

basic flowability

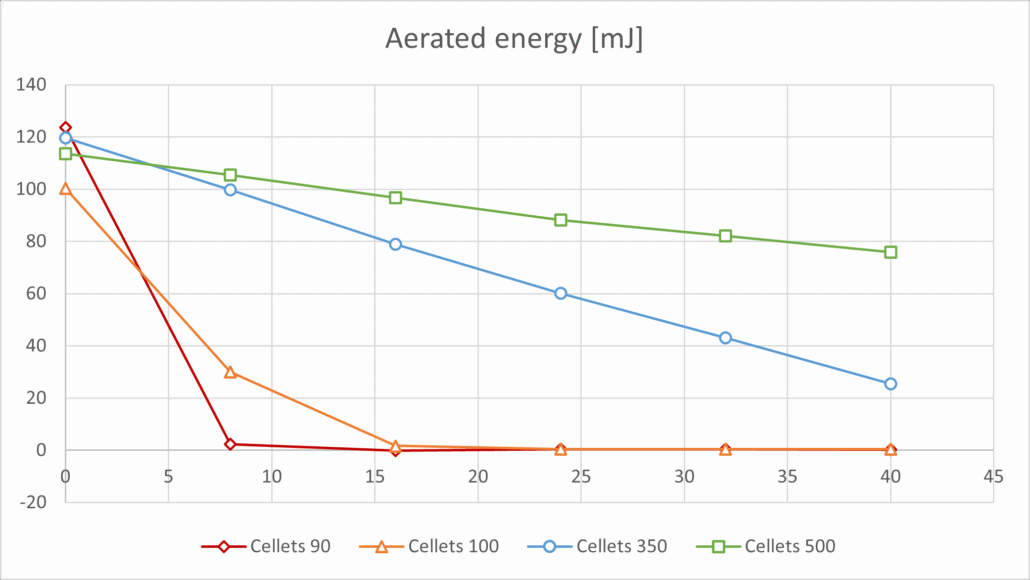
The aerated energy rises as air velocity decreases (Fig. 10). This parameter helps determine the minimum fluidization velocity, as increasing air velocity alters interparticle interactions.
aerated energy

The aerated energy increased with increasing pellet size (fig. 11). dependent on particle mass and inter-particle interactions (friction).

Mohylyuk 2022 MCC pellets under rheological investigation image 11 aerated energy size

with increasing pellet size, the cohesive index decreases (fig. 12). an indicator of the sum of inter-particle interaction forces.

12-cohesive index

Summary

Overall, researchers have now characterized MCC pellets under rheological investigation more comprehensively than ever before, providing new insights into their flow behavior and material properties. Powder rheology methods successfully revealed the bulk powder behavior, flow properties, and inter-particular interactions as a function of pellet size. CELLETS® served as robust model spheres made of Microcrystalline Cellulose, making them ideal for these detailed investigations. This study highlights the importance of pellet size in predicting and optimizing powder performance in pharmaceutical formulations.

References

[1] V. Mohylyuk and R. Dattani, “Assessment of the effect of microcrystalline cellulose (MCC) spheres size on the flow via powder rheology”, Conference: The FORGE: Hybrid Conference on Particle Characterisation (March 2022), doi:10.13140/RG.2.2.14935.75688

 

Characterization of Layered Pellets containing amorphized amlodipine besylate and hydrochlorothiazide

Characterization of layered pellets forms the basis of advanced pharmaceutical pellet design. These pellets consist of inert cores coated with active drug layers. Their detailed analysis ensures uniformity, strength, and consistent drug release. Layered systems offer precise dosing, extended or modified release, and taste masking. When the solid-state properties of the drug are modified through amorphization, the pellets can show faster dissolution and better bioavailability. In this study, researchers examined how a high-shear granulator can produce pellets that combine amorphized amlodipine besylate and hydrochlorothiazide, focusing on structure, performance, and stability.

Amlodipine besylate normally appears in a crystalline form with high solubility and a melting point near 200 °C. In contrast, hydrochlorothiazide is poorly soluble and melts near 270 °C. Turning them into an amorphous or co-amorphous form breaks down the crystal lattice, improving solubility and dissolution rate. In co-amorphous systems, the two drugs interact through hydrogen bonding, which stabilizes the amorphous state and prevents recrystallization. This interaction increases the dissolution of both drugs and enhances their bioavailability. The study found that partially amorphized drug mixtures in layered pellets improved release rates while maintaining physical stability.

A high-shear granulator creates these layered systems efficiently. Its strong mechanical forces and controlled heat allow uniform coating and induce amorphization at the same time. Because it works without solvents, this process is clean, fast, and suitable for sensitive compounds.

Summary of the Publication

In the study The Development and Characterization of Layered Pellets Containing a Combination of Amorphized Amlodipine Besylate and Hydrochlorothiazide Using a High-Shear Granulator, Mahmoud et al. [1] developed layered pellets by coating microcrystalline cellulose cores (CELLETS®) with drug mixtures in different molar ratios (2:1, 1:1, 1:2). The high-shear granulator (ProCepT 4M8) operated at 1,500 rpm and 60 °C for three hours. The goal was to achieve partial amorphization and study its impact on dissolution and stability. After preparation, the pellets were stored at –20 °C before testing.

Differential scanning calorimetry showed that amlodipine lost its sharp melting peak, confirming full amorphization. Hydrochlorothiazide retained a broad, weaker peak, meaning it was only partly amorphous. X-ray diffraction supported this: the 2:1 mixture had the lowest crystallinity (26.8 %), while the 1:2 mixture showed the highest (53.6 %). Micro-CT imaging revealed that the drug formed an even layer around the CELLETS® cores. Although some pores appeared, they were inherent to the cores rather than defects from coating.

Texture analysis indicated a small increase in hardness—from 19.8 N for plain CELLETS® to around 21 N for layered pellets—showing the coating slightly strengthened the structure. Dissolution testing showed moderate improvement for amlodipine and a strong improvement for hydrochlorothiazide, with release rates increasing up to 2.6 times. The faster release resulted from reduced crystallinity, improved wettability, and closer contact between drug and medium. FTIR spectra revealed broadening and merging of N–H peaks, confirming new hydrogen bonding and lattice disruption. Stability testing over one month showed that 2:1 and 1:1 ratios stayed mostly amorphous, while the 1:2 mixture recrystallized heavily.

Use of CELLETS® in This Study

The authors used CELLETS®, spherical microcrystalline cellulose cores about 1 mm in size, as the foundation for layering. Their smooth and strong surfaces ensured even coating under high shear. Micro-CT confirmed complete drug coverage and consistent thickness. Moreover, the CELLETS® provided the mechanical strength needed to prevent pellet fracture during processing. Their stable core structure helped maintain uniform shape and resistance to deformation.

Conclusion and Outlook

The study proves that solvent-free high-shear granulation can produce layered pellets with amorphized drug mixtures. The characterization of layered pellets showed lower crystallinity, faster release, and stable structure. Using CELLETS® as cores provided excellent mechanical support. The co-amorphous state of amlodipine and hydrochlorothiazide improved dissolution, especially for the poorly soluble hydrochlorothiazide.

Looking ahead, future research should test long-term stability under stress and evaluate in vivo bioavailability. Scaling the high-shear process could make it viable for industrial use. Furthermore, exploring multi-layer systems or combining more drugs could expand the possibilities of characterization of layered pellets in modern pharmaceutical development.

References

[1] Mahmoud et al., Pharmaceuticals 202518(10), 1496; doi:10.3390/ph18101496

Comparison of Mini-Tablets and Pellets as Multiparticulate Drug Delivery Systems for Controlled Drug Release

Multiparticulate Drug Delivery Systems: Advantages and Applications

Multiparticulate drug delivery systems offer clear advantages for controlled drug release. Manufacturers can place mini-tablets in hard capsules or administer them using special dosing units. Similarly, they can give pellets in hard capsules or compress them into tablets. Together, these forms provide flexible and precise drug delivery with polymer coatings.

In this study [1], researchers prepared four solid drug formulations and analyzed their drug release. First, they coated inert pellets with the model drug sodium benzoate. Next, they added a layer of insoluble ethyl cellulose. Afterward, they compressed the coated pellets into mini-tablets and normal tablets. Meanwhile, they directly compressed another type of mini-tablet from a sodium benzoate mixture and coated it with ethyl cellulose. They applied the coating using fluidized bed technology.

The coated pellets showed a lag time and retarded release. Afterward, the release followed first-order kinetics. In contrast, mini-tablets and normal tablets made from coated pellets released sodium benzoate without a lag time. This occurred because tableting partially disrupted the ethyl cellulose layer. Moreover, directly compressed mini-tablets released sodium benzoate more slowly as the coating thickness increased.

Therefore, the different formulations of coated pellets, mini-tablets, and normal tablets provide a wide range of drug release profiles. Consequently, they can meet various biopharmaceutical and pharmacological requirements.

Ethyl Cellulose-coated Mini-Tablets as Multiparticulate Drug Delivery Systems

Multiparticulate drug delivery systems can be made by compressing drug- and polymer-coated pellets into mini-tablets or normal tablets. Moreover, pellets and mini-tablets compressed into tablets spread widely in the small intestine. This improves drug absorption and increases bioavailability compared to normal tablets. In both tablet types, the sodium benzoate release slows down depending on the thickness and properties of the ethylcellulose coating.

Additionally, ethylcellulose-coated mini-tablets made by directly compressing sodium benzoate with excipients provide an alternative multiparticulate drug delivery method. These mini-tablets release the drug slowly, and the rate depends on the coating thickness. Consequently, they are suitable for prolonged-release applications. Furthermore, their release variation is higher than that of pellets or normal multiple-unit tablets made from pellets.

Finally, sodium benzoate layering on pellets using a fluidized bed, followed by tableting, works for both mini-tablets and normal tablets. Therefore, manufacturers can adjust the final pharmaceutical form to create diverse release profiles, which can support marketing or patenting strategies.

Read more

Read more about how CELLETS 200 are employed in mini-tablets and pellets as multiparticulate drug delivery systems by F. Priese et al.

Authors

F. Priese, D. Wiegel, C. Funaro, G. Mondelli, and B. Wolf, Coatings 202313(11), 1891; doi:10.3390/coatings13111891

Abstract

Pellets are one of multiparticulate pharmaceutical forms and can offer numerous technical and biopharmaceutical advantages compared with single dose unit formulations, e.g. tablets and capsules. This study aimed at formulation of controlled-release pellets of doxazosin mesylate (DM), a widely used treatment for antihypertensive and benign prostatic hyperplasia. DM was loaded onto microcrystalline cellulose CELLETS® pellets using hydroalcoholic solution and alcoholic suspension layering techniques to achieve a minimum drug load of 4 mg DM/g pellets. DM-layered CELLETS were coated by Aquacoat dispersion (ready-made ethylcellulose dispersion) using a coating pan technique as a simple and widely utilized technique in pharmaceutical industry. Controlled-release DM-layered pellets showed a release profile comparable to the controlled-release commercial product Cardura® XL Tablet. Also, the mechanism of DM release from Aquacoat CELLETS® was mathematically modeled and imaged by scanning electron microscopy to elucidate drug release mechanisms from the prepared pellet formulations. Accelerated stability studies of the prepared pellets were performed under stress conditions of 40 °C, and 75 % RH for 3 months. In conclusion, preparation of controlled-release DM-layered CELLETS® is feasible using a simple and conventional coating pan technology. Read more about controlled-release doxazosin mesylate pellets.

References

H. A. Hazzah, M. A. EL-Massik, O. Y. Abdallah & H. Abdelkader, Journal of Pharmaceutical Investigation (2013), 43:333–342. doi:10.1007/s40005-013-0077-0

Additional information

CELLETS® are perfect starter beads for coating and layering of API, such as doxazosin mesylate. Multilayer formulation attempts enable defined release profiles and improved bioavailability. Check different pellet sizes from 100 µm to 1400 µm which fit to your formulation.

Need formulation services?

Contact our partner Glatt Pharmaceutical Services!

Amorphous Solid Dispersions Layered onto Pellets - An Alternative to Spray Drying

This article “Amorphous Solid Dispersions Layered onto Pellets – An Alternative to Spray Drying?” is an excerpt from the publication of Neuwirth et al., Pharmaceutics 2023, 15(3), 764; https://doi.org/10.3390/pharmaceutics15030764.

Abstract

Spray drying is one of the most frequently used solvent-based processes for manufacturing amorphous solid dispersions (ASDs). However, the resulting fine powders usually require further downstream processing when intended for solid oral dosage forms. In this study, we compare properties and performance of spray-dried ASDs with ASDs coated onto neutral starter pellets in mini-scale. We successfully prepared binary ASDs with a drug load of 20% Ketoconazole (KCZ) or Loratadine (LRD) as weakly basic model drugs and hydroxypropyl-methyl-cellulose acetate succinate or methacrylic acid ethacrylate copolymer as pH-dependent soluble polymers. All KCZ/ and LRD/polymer mixtures formed single-phased ASDs, as indicated by differential scanning calorimetry, X-ray powder diffraction and infrared spectroscopy. All ASDs showed physical stability for 6 months at 25 °C/65% rH and 40 °C/0% rH. Normalized to their initial surface area available to the dissolution medium, all ASDs showed a linear relationship of surface area and solubility enhancement, both in terms of supersaturation of solubility and initial dissolution rate, regardless of the manufacturing process. With similar performance and stability, processing of ASD pellets showed the advantages of a superior yield (>98%), ready to use for subsequent processing into multiple unit pellet systems. Therefore, ASD-layered pellets are an attractive alternative in ASD-formulation, especially in early formulation development at limited availability of drug substance.

Materials

The model drugs ketoconazole (KCZ) and loratadine (LRD) were purchased from Sris Pharmaceuticals (Hyderabad, India). HPMCAS LG (hydroxypropyl-methylcellulose acetate succinate, wt%: methoxyl 20–24%, hydroxypropyl 5–9%, succinyl 14–18%; Mw = 18,000, HPMC-AS) was donated from Shin-Etsu Chemical (Tokyo, Japan). Eudragit L100-55 (methacrylic acid ethylacrylate copolymer, ratio 1:1, Mw = 320,000, EL100-55) was donated by Evonik (Darmstadt, Germany). Cellets 1000 (microcrystalline cellulose starter pellets, 1000–1400 µm) were provided by Glatt Pharmaceutical Services (Binzen, Germany). A detailed list of the pellets’ characteristics is shown in Table 1. Ethanol 96% (v/v) (technical grade) used in the sample preparation, and methanol (analytical grade) used for the HPLC analytics as well as the buffer salts disodium mono-hydrogen phosphate dodecahydrate (Na2HPO4·12H2O) and monosodium dihydrogen phosphate dodecahydrate (NaH2PO4·12H2O) were obtained from VWR Chemicals GmbH (Darmstadt, Germany).
Pellet Properties
d50 (xc min) [µm] 1123.44
(±7.36)
SPAN 0.166
(±0.002)
b/l 0.893
(±0.000)
SPHT 0.956
(±0.001)
Particle density [g/cm3] 1.452
(±0.016)
Sm [cm2/g] 36.41
(±0.29)

Table 1. Pellet properties of Cellets 1000. d50: mean particle diameter determined by the particle width; SPAN: width of the particle distribution; b/l: aspect ratio; SPHT: sphericity; Sm: specific surface area.

Pellet Coating (PC)
For pellet coating (PC) a laboratory scale fluid bed system Mini Glatt equipped with a Micro-Kit (Glatt GmbH, Binzen, Germany) was used. The coating was applied with a 0.5 mm two-fluid nozzle in bottom spray using the special bottom plate of the Micro-Kit to emulate a three-fluid nozzle with micro-climate. In the beginning, the machine was filled with 25.0 g of Cellets® 1000. The following process parameters were maintained throughout the process: Process gas flow 30 m3/h, product temperature 30.0 ± 1.0 °C (resulting inlet temperature 32–35 °C), spray pressure 1.5 bar and spray rate 1.0 ± 0.2 g/min. The final pellets had a theoretical drug-load of 10% (w/w) due to the fact that ASD and core pellets were used in a 1:1-ratio. […] To prepare the spraying solutions, the API and polymer were dissolved in ethanol 96% (v/v) under continuous stirring (solid content of 10% (w/w)). Prior to spraying, each solution was sonicated for 15 min to ensure complete dissolution of the components.
Subsequently, the coated pellets were manually sieved with a 2 mm mesh to eliminate multicore pellets. The pellets were dried under vacuum for 24 h at the same conditions as the SD powder.

Conclusions

In this study, we successfully prepared binary single phase ASDs of KCZ and LRD as weakly basic, slow crystallizing model APIs (drug load 20% (w/w)) using HPMC-AS or EL100-55 as pH-dependent soluble polymers via fluid bed pellet coating and spray drying. While the received ASD-pellets would not require further downstream processing other than capsule filling or tableting, the fine SD powder had to be transformed into dry granules. In combination with the slow crystallizers, KTZ and LOR, both manufacturing processes resulted in single-phased ASDs of high physical stability (up to 6 months) and similar dissolution performance when normalized to the total outer surface. The dissolution rate depends mainly on this total outer particle surface of the respective sample, independent of the manufacturing process, while the porosity of the sample had a minor impact on its dissolution behavior.
Especially for early formulation development, the high yield and ease of handling due to the pellet properties are strong advantages over the standard spray drying process. Nevertheless, the long process time in larger scale requires further process optimization in fluidized bed processing.
Amorphous solid dispersions Cellets 20230302

Figure: Amorphous solid dispersions.

[1] Neuwirth et al., Pharmaceutics 2023, 15(3), 764; https://doi.org/10.3390/pharmaceutics15030764

Abstract

This case study is a short abstract on spouted bed characteristics, following closely findings in the publication by J. Vanamu and A. Sahoo [1].

Spouted bed systems are of highest importance for all powder processing industries, and more specific in pharmaceutical industry for coating and drying in pellet technologies [2]. These systems offer manufacturing particularly fine and temperature-sensitive particles from small to large scale: laboratory systems are capable of processing product volumes of very few grams, while production systems can handle capacities of several tons [3].

But how to control conditions in spouted beds for efficient process applications, like mixing, coating, or drying?

There might be certain reasons, that the hydrodynamic behavior of the spouted bed in the pharmaceutical industries is less investigated. The referred publication shed some light on the hydrodynamic characteristics of a spouted bed where the MCC Spheres (CELLETS®) are adopted as the bed material. These starter cores are ideal model systems due to their perfect sphericity and zero-level friability. At the same time, smooth and defined surface structure initiate perfect modelling conditions in the spouted bed dynamics.

Material

CELLETS®, made of 100% Microcrystalline Cellulose, have been used as bed material. The physical properties of the CELLETS® are shown in Table 1. The CELLETS® particle morphology is represented in Figure 1.

Parameter Value
CELLETS® 700 and CELLETS® 1000
Size distribution 700-1000 µm (CELLETS® 700)

1000-1400 µm (CELLETS® 1000)

Bulk density 800 kg/m3
Particle sphericity > 0.9
Void fraction 0.42
Geldart classification B

Table 1: Physical properties of the CELLETS®.

SEM micrographs of CELLETS® 700

Figure 1: SEM micrographs of CELLETS® 700, found in [1].

Spouted bed: experiment setup

There are some international players on the market of spouted bed technologies, such as Glatt which seems to be the major one (Figure 2). In this framework, a self-made setup is used for experiments. The experiments that have been carried out in a column, which is fabricated from a Perspex sheet. This column consists of a cylindrical section of height 0.53 m and a diameter of the cylinder of 0.135 m. The column further converged the diameter of the cylinder to 0.05 m as a conical bottom having a length of 0.47 m. The spouting air is supplied by a compressed air line is controlled by a gas regulator. The airflow is controlled by a gate valve and a mesh plate having a mesh size less than the size of the bed material is employed as a separator preventing the backflow of the bed material. Images are captured using a high-speed video camera to gain more details of the hydrodynamic characteristics of the flow pattern inside the spouted bed geometry.

Spouted bed

Figure 2: Scheme of a spouted bed (Glatt, Germany).

Experiments & spouted bed results

Experiments are carried out with three different static bed heights of shallow depth wherein the bed height is in the range of factor 2-3 of the Inlet diameter using two different particle distribution classes at 500-710 µm and 700-1000 µm, respectively. Analyzed parameters are the pressure drop across the bed, the bed expansion ratio, and the clusters concerning the superficial gas velocity are focused in the following.

J. Vanamu et al. found that the “bed expansion ratio increases with increasing superficial gas velocity until the onset of external spouting, further increase in the superficial gas velocity, the bed expansion ratio decreases. With increasing the volume of bed, the bed expansion ratio decreases. In a larger volume of bed, the particles tend to spout into the freeboard region rather than expanding with higher superficial gas velocity”. Initial spouting is symmetric, but with increasing superficial gas velocity spouting becomes asymmetric, and asymmetry is more pronounced or starts at lower superficial gas velocities for smaller particles. This agrees with existing theories of hydrodynamic behavior in a fluidized environment. Respecting the necessarity of a proper flow behavior for mixing, coating or drying applications in drug processing, symmetric spouting is essential. In turn, the superficial gas velocity may be kept low.

In case that high superficial gas velocity regimes are required for the operations a draft tube may be installed within the column to achieve the symmetric spout formation.

Summary

This case study highlights the Hydrodynamic behavior of MCC spheres in a spouted bed using image processing method. MCC spheres in the range between 500-710 µm and 700-1000 µm had been employed. All spheres showed a symmetric and asymmetric spouting in the spouted bed. With increasing superficial gas velocity, the fully suspended particles are limited to a certain height in the freeboard region due to the gas-solid crossflow. A change from symmetric to asymmetric spouting is observed with increasing superficial gas velocity.

Keeping the conditions efficient for the mixing, coating or drying applications requires finally to suppress high superficial gas velocities, or changing the setup in such way, that symmetric spouting conditions are kept upright even at higher superficial gas velocities.

References

[1] J. Vanamu and A. Sahoo, Particuology 76 (2023) 101

[2] L. A. P. de Freitas, Particuology 42 (2019) 126

[3] Glatt GmbH, Binzen, Germany. Online on Nov 8, 2022: Spouted bed systems – Glatt – Integrated Process Solutions

Great thanks to Arihant Innochem Pvt. Ltd. who supplied and donated CELLETS® for this study.

Abstract

Multiparticulates made of pellets are ideal dosage forms to be used in pediatrics. Having the suitability of paediatric consumers in mind, formulations of small-sized pellets offer a valuable base for increased compliance and improved age-appropriately dosage form. Due to their round shape of pellets, smooth surface area and narrow particle size distribution they can easily be functionally coated [1] to achieve e. g. a taste masking, enteric protection or the controlled release of the active pharmaceutical ingredient (API) in defined parts of the gastro-intestinal (GI) tract. The release profile then often depends on the coating weight gain (thickness) and composition of the functional coating.

Coating weight gain, manufacture and analysis of pellets

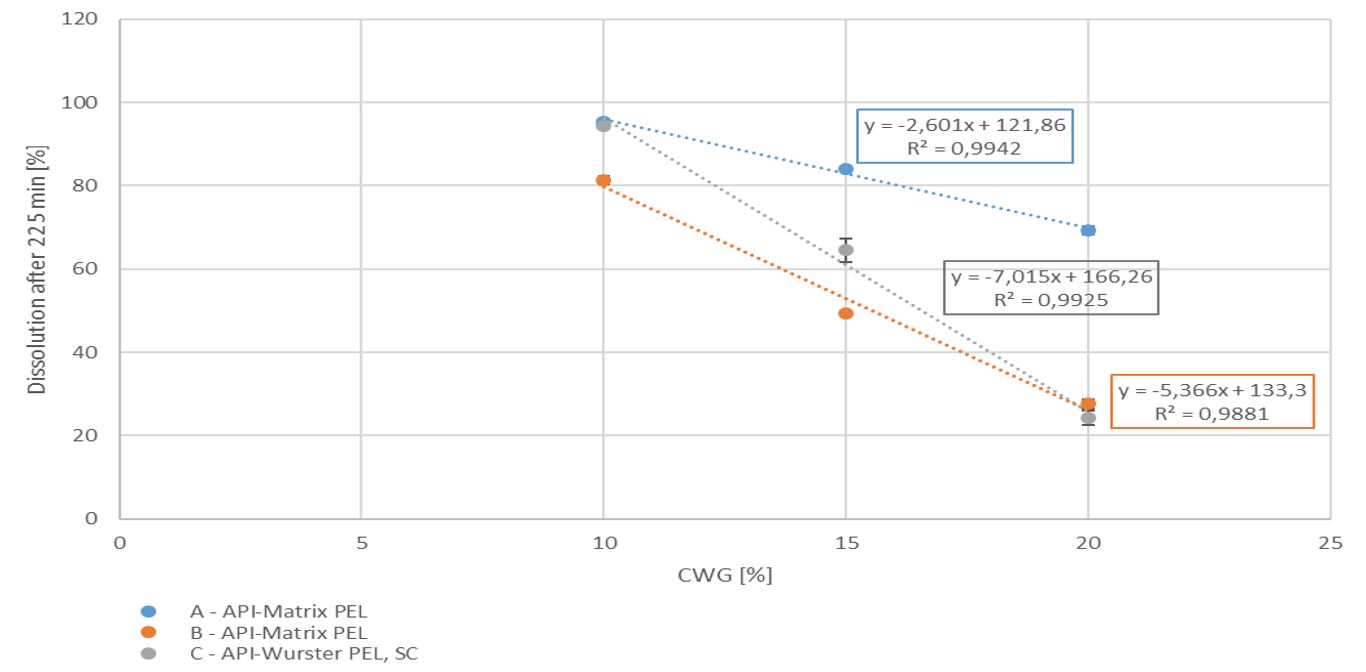
A well soluble drug was used as model API.  In a first approach, pellets were produced applying the ProCell technology, a direct pelletization process allowing the production of highly drug loaded matrix pellets (here 95%) in a spouted bed. Two types of pellets were produced: A) with a poly amino saccharide-based binder, followed by a cellulose based seal coating and B) with a polyacrylic acid-based binder, followed by a pH-depending coating. In a second approach the API was layered onto inert starter cores (MCC, CELLETS® 200) by the aid of a cellulose based binder and antitacking agent applying the Wurster technology targeting a drug load of 50 %, followed by a pH-depending coating (C). All three pellets-based populations were functionally coated by a pH-independent sustained release polymer. Samples were taken at pre-defined coating levels for dissolution testing. For API layering and coating a GPCG 1.1 with a 6” Wurster insert was used. Direct pelletization was performed in a ProCell 5. Particle size distribution (PSD) analysis was performed by Eyecon2TM. The particle size is given as numeric or volumetric distribution (e.g. Dn50 or Dv50). The specific surface area is calculated by measuring the true density by gas pycnometry and the Sauter diameter by Laser diffraction. Dissolution was measured in the acid stage (0.1 M HCl), in buffer pH 5.5 and in buffer pH 7.2 over 300 min. The API should not be released in the first 180 min. Between 210 min and 240 min an increased drug release is expected. The dissolution rates at 225 min were compared for the coating levels at 10, 15 and 20 %.

Results

With increasing coating weight gains decreasing dissolution rates at 225 min were measured for the sustained release coating with a good linearity. Matrix PEL (A) show higher dissolution rates comparing the same coating levels than Matrix PEL (B), Wurster pellets showed the strongest decrease with increasing CWG, table 1, figure 1. This correlation was not observed for pH-depending coating (data not shown).

Dv 50 [µm] Dn 50 [µm] PSD mean [µm] Specific surface area [m2/g]
A Matrix PEL 496 475 481 0,00980
B Matrix PEL 461 427 425 0,01210
C Wurster PEL 414 396 401 0,01100

Table 1. PSD data and specific surface area of starter beads before functional coating.

coating weight gain

Figure 1. Dissolution at 225 min vs. coating weight gain (CWG)

Summary

Drug loaded pellets were prepared either as matrix pellets applying the ProCell technology, or by layering of starter cores applying the Wurster technology. Both populations were coated with different coating levels of a sustained release functional coating, resulting in decreasing dissolution rates with increasing coating weight gain. Due to the good correlation between coating weight gain and dissolution profile a prediction of the dissolution rate might be possible for pre-defined coating levels. These findings are a crucial step towards novel paediatric formulations with improved dissolution profiles and dosage safety.

References

[1] Palugan, L.; Cerea, M.; Zema, L.; Gazzaniga, A.; Maroni, A. Coated pellets for oral colon delivery, Journal of Drug Delivery Science and Technology 25, 1 – 15 (2015).

This study was presented on 14th annual EuPFI conference, Rome, Italy.

Figure 3: SEM picture of cross section of a Taste masked pellets coated with 25 mg Eudragit EPO.

Abstract

This case study on Atomoxetine HCl pellets is a short abstract of the publication by Y.D. Priya et al. [1].

Atomoxetine is a medication used to treat attention deficit hyperactivity disorder (ADHD) [2]. The API is marketed under the trade names Atomoxetine, Atomoxe, Agakalin, and Strattera (initially launched) [3]. Atomoxetine is an extremely bitter API. As being initially launched for children as capsules or tablets, the paediatric compliance by improved taste-masking and the simplified administration to paediatrics are in focus of this study.

A multi-unit particulate pellet coating (MUPS) was selected as oral dosage form. The fluidized bed technology (with Wurster column) was employed for coating and layering processes. This is a well-known technology, which Is for instance offered by Glatt. Starter cores were coated with the API, followed by layering with a polymeric coating for which realized the taste-masking.

Atomoxetine layering

Starter cores are made of Microcrystalline Cellulose (MCC) in sizes comparable to CELLETS® 200, while a fair efficiency of drug layering was observed with the combination of HPMC (Hydroxypropyl methyl cellulose) and HPC (Hydroxypropyl cellulose) as binders. The composition of API layering is presented in Table 1. The drug dispersion was sprayed onto the MCC pellets with an inlet temperature between 50 °C and 55 °C and a fluidized bed temperature between 35 °C and 40 °C.

API layering material Composition
Starter core
  MCC pellets 58.00
API layering
  Atomoxetine HCl 25.00
  Hydroxypropyl methylcellulose 3.50
  Hydroxypropyl Cellulose 3.50
  Low-Substituted Hydroxypropyl Cellulose 5.00
  Talc 5.00
  Purified Water Qs
Total weight (mg) 100.00

Table 1: Formulation of API layered pellets.

Taste-masking coating

The polymeric taste-masking layer is made of a methacrylate co-polymer (Eudragit EPO) providing an excellent coating with taste masking properties for fine particles and tablets. The composition of the taste-masking suspension is shown in Table 2. The inlet temperature is between 40 °C and 45 °C, and fluidized bed temperature is between 25 °C and 30 °C.

Polymeric coating material Composition
Drug Layered pellets 100.00
Eudragit EPO 25.00
Sodium Lauryl Sulfate 2.500
Stearic acid 3.750
Talc 6.25
FD&C Yellow No. 6 0.50
FD&C Red No. 3 0.05
Purified Water Qs
Total weight (mg) 138.050

Table 2: Formulation of polymeric coating suspension.

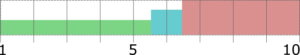
The efficiency of taste-masking was benchmarked by a bitterness rating on human volunteers. Figure 1 shows, that the taste sensitivity identifies a bitterness at 6 µg/ml API concentration and an extreme bitterness at 7 µg/ml API and higher concentration. Thus, the threshold bitterness of Atomoxetine HCl is 6 µg/ml.

Atomoxetine: bitternessFigure 1: Concentration of drug solution (µg/ ml). Bitter intensity ratings from no bitterness (green), bitterness (blue), extremely bitter (red).

Figure 1: Concentration of drug solution (µg/ ml). Bitter intensity ratings from no bitterness (green), bitterness (blue), extremely bitter (red).

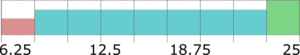
All the volunteers felt bitter taste when the drug layered pellets were coated with 6.25 mg of Eudragit EPO. Whereas in the pellets coated with 12.5 mg and 18.75 mg of Eudragit EPO, bitter taste was masked up to 15 seconds after keeping the tablet in the mouth, and later all the human volunteers felt bitter taste. When the concentration of Eudragit EPO was increased to 25 mg, the bitter taste of Atomoxetine HCl was completely taste-masked and no volunteer was felt bitter taste.

Figure 2: In-Vivo Taste evaluation in healthy human volunteers.

Figure 2: In-Vivo Taste evaluation in healthy human volunteers.

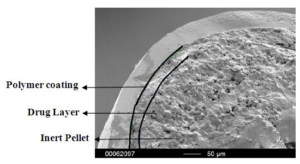
Figure 3 depicts the entire particle size of a taste-masked MCC pellet coated with the Atomoxetine drug layer and 25 mg of Eudragit EPO. The average particle size of the taste-masked pellets is between 180 µm and 250 µm, assuming, that no gritty feeling of particles in patient’s mouth will appear. It should be said, that a micronization of Atomoxetine HCl was deemed to be necessary for the drug layering process. Micronization minimized the surface roughness of the API layered pellet so that an efficient taste-masking coating can be applied.

Figure 3: SEM picture of cross section of a Taste masked pellets coated with 25 mg Eudragit EPO.

Figure 3: SEM picture of cross section of a Taste masked pellets coated with 25 mg Eudragit EPO.

Summary

MCC pellets in the size of about 200 µm were layered with Atomoxetine. HPMC and HPC were used as binders, realizing a precise surface definition for a subsequent taste-masking coating. The taste-masking was most efficient at a polymeric concentration of 25 mg. Keeping the size of the coated pellets below 300 µm avoids a gritty feeling and thus increase the patient’s compliance.

This study by Priya et al. indicated that the fluidized bed process produced the most appropriate taste masked pellets of Atomoxetine HCl for oral disintegrating tablets.

References

[1] Y.D. Priya et al., Int J Pharm Pharm Sci, (6) 7, (2014) 110-115

[2] “Atomoxetine Hydrochloride Monograph for Professionals”. Drugs.com. American Society of Health-System Pharmacists. Archived from the original on 4 April 2019. Retrieved 22 March 2019.

[3] ROTE LISTE 2017, Verlag Rote Liste Service GmbH, Frankfurt am Main, ISBN 978-3-946057-10-9, (2017) 162.

Close-up SEM images of Cellets® 500 particles coated with sodium benzoate at process conditions as printed in Table 2 (bold).

Abstract

Multidimensional Correlation of Surface Smoothness and Process Conditions is a necessary attempt to better understand, optimize and outperform process steps of drug formulations. Particle coating and layering in a fluidized bed process is a main attempt in pharmaceutical industry for drug production for modern oral dosage forms. The precise knowledge of control process parameters leads to high surface control of the drug-loaded particles and therefore is crucial for the quality and yield of production in a more general aspect. This application note presents a multidimensional attempt by Orth et al. [1] to correlate particle surface structure morphology and process conditions in a fluidized bed layering spray granulation. CELLETS® 500 are used as spherical, high-quality starter cores.

About fluidized bed process conditions

Fluidized bed processes are used in pharmaceutical, food and agro industries. Solid particles are transported in a defined gas stream inducing fluidized bed conditions. Solid-containing dispersions or liquids are sprayed onto the fluidized particles. Variable settings of process parameters allow particle layering, coating, coalescence and agglomeration. This point seems to make the fluidized bed becoming a universal process for particle processing, but also requests deeper knowledge about the desired process parameter settings: The goal is a stable, high-quality, high-output process.

Standard process parameters are:

  • liquid spray rate (m­1)
  • fluidization air flow rate (Vair)
  • fluidization air temperature (Tin)
  • spray air temperature (Tat)
  • spray atomization pressure (at)

Beside the spraying process, also the drying process plays an important role. By drying, moisture, sticky conditions and flowability are strongly influenced. Hampel [2] analyzed in her doctoral thesis the importance of the drying process using CELLETS® 200 as model particles.

Technology, Materials and Analysis

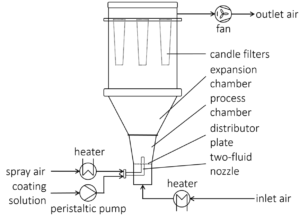
The coating experiments were carried out in a ProCell® 5 LabSystem with the fluidized bed process chamber GF3 (Glatt GmbH, Germany) as shown in Figure 1. The ProCell® 5 LabSystem is designed for testing of spouted bed and fluidized bed processes in the single kg-scale.

Sketch of the experimental fluidized bed setup (Procell® 5 LabSystem with GF3 chamber).

Fig.1: Sketch of the experimental fluidized bed setup (Procell® 5 LabSystem with GF3 chamber).

As Materials, pellets made of 100% microcrystalline cellulose (CELLETS® 500) are employed as perfect starter cores. These pellets provide smooth and defined surface properties, chemical inertness, robustness and a high degree of sphericity. Specific properties of CELLETS® 500 for this study are shown in Table 1. The roughness is at 1.5 µm and therefore delivers perfect initial conditions for controlled spray granulation.

Property Value
Sauter diameter 639 µm
Sphericity 0.96
Surface roughness 1.5 µm
Solid density 1.445 g/cm3

Table 1: Properties of CELLETS® 500.

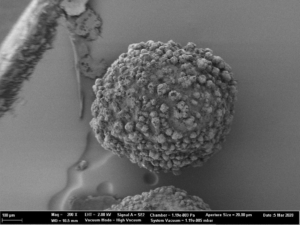
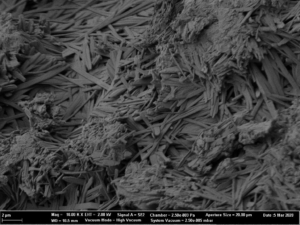
As spray liquid, a 30 wt% sodium benzoate solution was injected into the process chamber. The mass ratio of spray liquid to starter cores was 1:2. Different coating conditions have statistically been driven. In turn, the spray-coated particles show different surface structures (Figure 2a-d).

SEM images of Cellets® 500 particles coated with sodium benzoate at process conditions as printed in Table 2 (bold).

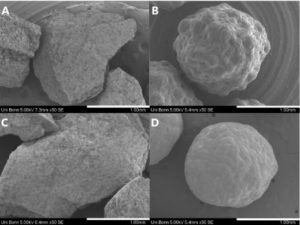
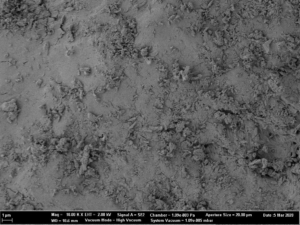
Fig.2a: SEM images of CELLETS® 500 particles coated with sodium benzoate at process conditions as printed in Table 2 (bold).

Close-up SEM images of Cellets® 500 particles coated with sodium benzoate at process conditions as printed in Table 2 (bold).

Fig. 2b: Close-up SEM images of CELLETS® 500 particles coated with sodium benzoate at process conditions as printed in Table 2 (bold).

SEM images of Cellets® 500 particles coated with sodium benzoate at process conditions as printed in Table 2 (italic).

Fig. 2c: SEM images of CELLETS® 500 particles coated with sodium benzoate at process conditions as printed in Table 2 (italic).

Close-up SEM images of Cellets® 500 particles coated with sodium benzoate at process conditions as printed in Table 2 (italic).

Fig. 2d: Close-up SEM images of CELLETS® 500 particles coated with sodium benzoate at process conditions as printed in Table 2 (italic).


Parameter Controlled values
liquid spray rate (m­1) 10 | 15 | 20
fluidization air flow rate (Vair) 80 | 105 | 130
fluidization air temperature (Tin) 50 | 85 | 120
spray air temperature (Tat) 20 | 70 | 120
spray atomization pressure (at) 0.5 | 1.75 | 3.0

Table 2: Process parameters and values used in coating experiments.

The coated particles were analyzed regarding their surface roughness via laser scanning microscopy (VK-X160K, Keyence, Japan). Additional images were obtained with a scanning electron microscope (Supra VP55, Zeiss, Germany).

A 3D-profile of the particle surface was created and evaluated in a defined measurement area. Roughness analysis can be performed through several parameters as defined in DIN EN ISO 4287:2010-07 (2010) and DIN EN ISO 25178-2:2012 (2012). In this attempt, the arithmetical mean height was used as roughness quantifier. The roughness was correlated to the process parameters and the resulting linear correlation was rigorously analyzed using a principal component analysis.

Results

A linear regression model is fitted to the roughness data using the ordinary least squares method. This enables to create a linear model connecting the chosen process parameters to the surface roughness of the coated particles. It is mentionable, that in this attempt the fluidization air flow rate and the spray air temperature did not show a significant effect on the surface structure and were therefore removed from the model.

Process conditions: Influence of the liquid spray rate

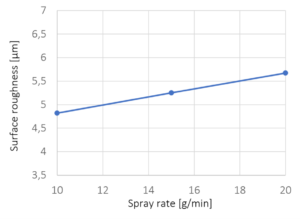
Figure 3: Surface roughness versus liquid spray rate. The crosses mark the experimentally investigated spray rates; line represents a linear interpolation.

Figure 3: Surface roughness versus liquid spray rate. The crosses mark the experimentally investigated spray rates; line represents a linear interpolation.

The dependence of the surface roughness on the spray rate of the sodium benzoate solution is shown in Figure 3. A slight increase of surface roughness is identified for increasing spray rates. The main effect is considered to be influenced by the crystallization of sodium benzoate. Following, crystallization is higher at higher spray rates caused by lower evaporation due to higher liquid volumes in the process. The dependence of the crystallization of sodium benzoate on the drying conditions during fluidized bed coating was also observed by Rieck et al. [3] and Hoffmann et al. [4].

Process conditions: Influence of the fluidization air inlet temperature

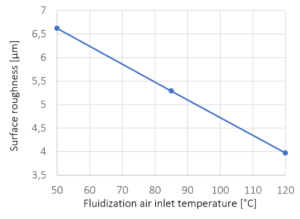
Figure 4: Surface roughness versus fluidization air inlet temperature. The crosses mark the experimentally investigated temperatures; line represents a linear interpolation.

Figure 4: Surface roughness versus fluidization air inlet temperature. The crosses mark the experimentally investigated temperatures; line represents a linear interpolation.

An increase in the fluidization air inlet temperature results in a lower roughness of the coated particles and therefore in a smoother particle surface. The temperature of the fluidization air has a major impact on the drying conditions during the spray granulation process. As an increased temperature causes reduced relative humidity, the heated air can absorb a larger amount of water, which results in a high drying rate. Crystal growth of spray droplets is reduced by fast evaporation times and short drying times.

Process conditions: Influence of the atomization pressure

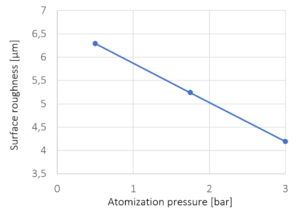
Figure 5: Surface roughness versus spray atomization pressure. The crosses mark the experimentally investigated pressures; line represents a linear interpolation.

Figure 5: Surface roughness versus spray atomization pressure. The crosses mark the experimentally investigated pressures; line represents a linear interpolation.

With increasing atomization pressure from 0.5 bar to 3.0 bar, the surface roughness is decreasing. The pressure of the spray air strongly influences the droplet size and velocity. With increasing atomization pressure, the droplet size and size distribution decreases while the droplet velocity increases which in causes a more homogeneous spreading and promotes smoother surface coatings.

Summary

CELLETS® 500 are used as model particles for analyzing the surface roughness of coated particles dependent on process conditions in a bottom-spray process. As the results suggest, a high surface roughness is achieved at low fluidization air temperatures, low atomization pressures and high spray rates of the coating solution. Conversely, at high air temperatures, high spray pressures and low liquid spray rates, particles with smooth and compact surfaces are produced.

Acknowledgement

Prof. Stefan Heinrich and his team are gratefully acknowledged for serving content for this note:

Hamburg University of Technology - Institute of Solids Process Engineering and Particle Technology
Hamburg University of Technology
Institute of Solids Process Engineering and Particle Technology
Contact: Prof. Dr. Stefan Heinrich
Denickestrasse 15, 21073 Hamburg, Germany
Tel: +49 40 42878 3750
E-mail: stefan.heinrich@tuhh.de
Website: https://www.tuhh.de/spe/

The authors got funding from the German Research Foundation within the DFG Graduate School GRK 2462 “Processes in natural and technical Particle-Fluid-Systems (PintPFS)” (Project No. 390794421) and funding from BASF SE.

CELLETS® 500 were sponsored by HARKE Pharma.

References

[1] M. Orth, P. Kieckhefen, S. Pietsch and S. Heinrich. KONA Powder and Particle Journal (2021). DOI: 10.14356/kona.2022016

[2] N.A. Hampel, Dissertation, Otto-von-Guericke-Universität Magdeburg, 2015. DOI:10.25673/4340

[3] Rieck C., Hoffmann T., Bück A., Peglow M., Tsotsas E., Powder Technology, 272 (2015) 120–131. DOI:10.1016/j.powtec.2014.11.019

[4] Hoffmann T., Rieck C., Bück A., Peglow M., Tsotsas E., Procedia Engineering, 102 (2015) 458–467. DOI: 10.1016/j.proeng.2015.01.189